Metal Detector Sensitivity Limits: What Spec Sheets Hide
1. Introduction: The Gap Between Lab Certification and Line Reality
It is 4:00 PM on a Friday. Your quality assurance team has just finished running standard calibration checks across your packaging line. The test pieces—1.0 mm Ferrous, 1.2 mm Non-Ferrous, and 1.5 mm Stainless Steel 316 spheres—passed cleanly through the aperture, triggering the pneumatics every single time. The HACCP audit log registers 100% compliance.
Yet, three weeks later, a key distribution partner flags a batch: an ultra-thin stainless steel cutting wire snippet, measuring less than 0.4 mm in diameter, was discovered inside a sealed bag.
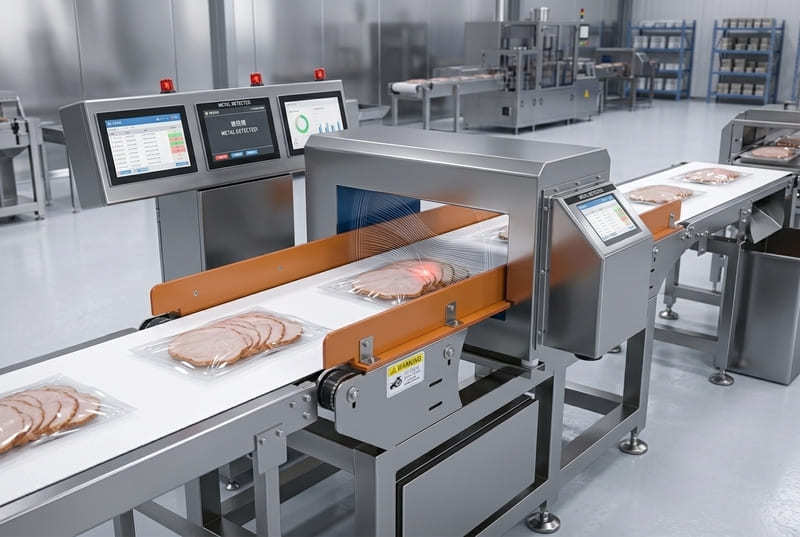
How does a fully calibrated industrial inspection system, operating within its stated specification sheet parameters, miss a foreign object that seems large enough to see with the naked eye?
This uncomfortable scenario is far more common in high-speed manufacturing than equipment spec sheets suggest. Plant managers and QA directors frequently fall into the trap of treating a metal detector’s "spherical sensitivity" as an absolute guarantee of real-world contaminant interception. In reality, an equipment datasheet reflects optimal, laboratory-grade performance under zero-noise conditions.
On an active conveyor belt, electromagnetic inspection is governed by the unyielding laws of physics. Understanding the gap between ideal lab sensitivity and actual line interception rate is the first step toward building a truly audit-ready, zero-defect packaging line.
2. The "Test Sphere" Paradox: Why Geometry Masks Real-World Hazards
To understand why real contaminants slip past inspection, one must first look at how sensitivity is measured across the industry. Equipment manufacturers quantify performance using precision-ground test spheres made of Ferrous (Fe), Non-Ferrous (Non-Fe, typically Brass), and Stainless Steel (SS 316).
Spheres are chosen as the universal calibration benchmark for a simple reason: geometry. A sphere presents an identical electromagnetic cross-section regardless of its orientation, velocity, or angle of approach through the detection coil. It represents a perfectly symmetrical disturbance in the high-frequency magnetic field.
However, industrial contaminants in processing environments rarely enter the line as convenient round beads. They appear as:
● Wire strands from wire-mesh conveyor belts
● Flakes from worn processing blades
● Slag or metal shavings from upstream maintenance
● Broken needles or processing pins
The Orientation Effect
When a non-spherical object—such as a piece of fine wire—passes through an active magnetic field, its detectability drops dramatically depending on its orientation relative to the field lines. This phenomenon is known as the Orientation Effect.
[Direction of Field Lines]
↓ ↓ ↓ ↓
======================== ← Wire Parallel to Field Lines
(Minimal Cutting of Magnetic Flux → WEAK SIGNAL)
↓ ↓ ↓ ↓
| | ← Wire Perpendicular to Field Lines
| | (Maximum Cutting of Magnetic Flux → STRONG SIGNAL)
========================
If a 0.4 mm diameter stainless steel wire passes through the aperture perpendicular to the magnetic field, it cuts across a large density of magnetic flux lines, generating a strong eddy current that triggers the alarm. However, if that exact same 0.4 mm wire passes through parallel to the field lines, its effective magnetic cross-section is reduced solely to its 0.4 mm end profile.
To the detector coil, a 20 mm long wire traveling in a parallel orientation generates a signal no larger than a 0.4 mm sphere—well below the physical threshold of a machine calibrated to detect 1.5 mm SS 316 spheres. This physical reality explains why a line can pass every spherical test piece while remaining vulnerable to thin metal slivers.
For operations seeking to bridge this gap, selecting robust conveyor metal detectors engineered with advanced digital signal processing is essential to extracting maximum signal clarity from weak orientation profiles.
3. The 3 Hard Physical Constraints in Industrial Metal Detection
Beyond contaminant geometry, three fundamental physical constraints dictate the limits of inline metal inspection. Ignoring these variables during equipment selection inevitably leads to false rejects, missed contaminants, or costly line downtime.
| Physical Constraint | Physical Mechanism | Impact on Detection | ||
| Aperture Size | Field strength decays rapidly toward the geometric center of the opening. | Oversized apertures cause severe sensitivity "valleys" at the tunnel core. | ||
| Metallurgy | SS 316 lacks magnetic permeability and has low electrical conductivity. | Requires 1.5× to 2.0× larger sphere diameter to detect compared to Ferrous metals. | ||
| Product Effect | High moisture, salt, or acidity generate conductive phase shifts. | Creates false reject signals, forcing operators to manually reduce machine sensitivity. | ||
Constraint 1: Aperture Sizing & Center-Field Decay
An industrial metal detector operates via a three-coil system housed within a rigid frame. A central transmitter coil radiates a high-frequency electromagnetic field, while two adjacent receiver coils measure the balance of the induced field.
By the laws of electromagnetism, field strength is concentrated nearest to the internal walls of the enclosure aperture. As you move toward the geometric center of the opening, the field strength decays significantly.
● The Edge Effect: A contaminant passing 10 mm away from the top coil generates a strong, crisp signal.
● The Center-Field Decay: The exact same contaminant traveling through the geometric center of the tunnel generates the weakest possible signal.
Plant engineers often order oversized apertures to allow a single conveyor line to handle multiple package heights. However, doubling the aperture height does not merely decrease sensitivity proportionally—it causes an exponential reduction in center-field magnetic intensity.
Constraint 2: Metallurgy & Electromagnetic Phase Shift
Not all metals disturb an electromagnetic field equally. The physical response of a metal particle depends on two distinct properties: magnetic permeability and electrical conductivity.
● Ferrous Metals (Fe): Highly magnetic and electrically conductive. They easily distort the magnetic field and produce strong, high-amplitude disturbance signals.
● Non-Ferrous Metals (Brass, Copper, Aluminum): Non-magnetic but exceptionally conductive. They create strong secondary eddy current fields that disturb the receiver coils via phase displacement.
● Stainless Steel (SS 316): Non-magnetic and possesses poor electrical conductivity. Because SS 316 produces neither a strong magnetic distortion nor a large eddy current, it is the most difficult material to detect.
On average, a system capable of detecting a 1.0 mm Ferrous sphere will require a 1.2 mm Non-Ferrous sphere and a 1.5 mm to 2.0 mm SS 316 sphere to generate an equivalent signal voltage.
Constraint 3: The "Product Effect" (Conductive Interference)
Perhaps the most frustrating challenge in quality control is the Product Effect. High-moisture, high-salt, or highly acidic products—such as fresh poultry, block cheese, warm bakery items, and ready-to-eat meals—possess high electrical conductivity.
When these conductive items pass through the high-frequency search head, they behave like massive, weak metal contaminants. They generate a signal known as a "Phase Shift."
If the detector is tuned to extreme physical sensitivity, the product signal itself triggers the rejection mechanism, creating unacceptable numbers of false rejects. To prevent high product waste and constant line stoppages, frustrated operators often manually lower the machine's overall sensitivity—effectively blinding the machine to real metal fragments.
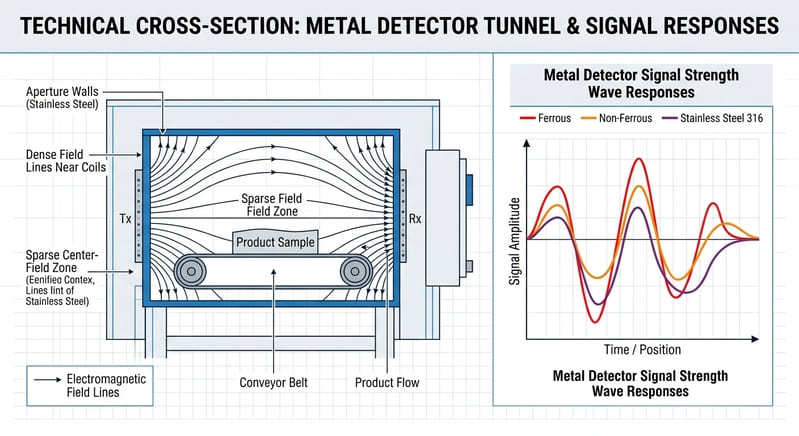
Understanding these trade-offs is particularly critical when designing food industry inspection solutions for high-moisture production environments.
4. Engineering Action Plan: Overcoming Physical Limits on Your Conveyor Line
While you cannot rewrite Maxwell’s equations, modern industrial engineering provides actionable strategies to mitigate these physical barriers and maximize real-world interception.
Strategy 1: The Minimal Aperture Principle
Always size the detector head around the maximum physical profile of the product, not around the width of the room. Maintaining a tight 20 mm to 30 mm clearance above the top of the highest product container minimizes the weak center-field zone, maximizing signal-to-noise ratio (SNR) across the entire belt width.
Strategy 2: Multi-Frequency Phase Suppression & Auto-Learn
Legacy analog systems relied on fixed, single-frequency operation, forcing plants to compromise between sensitivity and product effect suppression. Modern digital architecture utilizes multi-frequency spectrum analysis and automated product learning.
At SameGram, our conveyor metal detectors incorporate intelligent auto-learn software algorithms. The system scans the product across multiple frequency spectrums during set-up, mapping the unique phase angle signature of conductive moisture or salt content. It then establishes an adaptive threshold curve that mathematically cancels out the product effect signal without suppressing the distinct frequency spike generated by genuine metal contaminants.
Strategy 3: Multi-Inspection Synergy (Combination Systems)
For lines handling metallized film packaging, aluminum foil trays, or ultra-dense frozen blocks, conventional electromagnetic fields face severe physical boundaries. In these specialized applications, relying on a single inspection methodology is insufficient.
High-efficiency lines increasingly combine metal detection with dynamic weight monitoring or transition to advanced high-density imaging:
● Integrated Weighing & Inspection: Combining dynamic weight checking with metal detection into a single footprint ensures both weight compliance and foreign object interception. Explore integrated dynamic checkweighers and space-saving combination weighing and inspection systems to streamline line layout.
● X-Ray Foreign Object Detection: When products are wrapped in heavy aluminum foil or require detection of glass, bone, or stone alongside metal, X-ray inspection systems bypass electromagnetic phase limits entirely by inspecting based on material density differences.
5. Built for Compliance: Quality Assurance You Can Audit
In modern manufacturing, an inspection system is only as good as its compliance credentials. Regulatory frameworks across food processing, personal care, and pharmaceutical and health product applications require verifiable equipment safety and electromagnetic compatibility.
To ensure your facility remains fully audit-ready under international quality standards, SameGram equipment is built and certified to rigorous global standards:
● Harmonized Safety & EMC Compliance: Fully certified under European health, safety, and environmental directives via our official SameGram EMC+MD+LVD Certification.
● Hazardous Substance Restriction: Manufactured with environmentally safe, non-hazardous components verified by our official SameGram Conveyor Metal Detector ROHS Certification.
By integrating IP69K washdown-rated construction, tool-less belt disassembly, and automated data logging, these systems ensure your plant maintains HACCP, BRC, and FDA compliance without slowing down production throughput.
6. Partnering with SameGram: Engineering Precision for Your Facility
At SameGram Equipment Co., Ltd., we believe that effective quality control starts long before a machine is installed on your factory floor. We don't sell generic off-the-shelf machinery; we deliver tailored, intelligent detection solutions built around your exact product characteristics, line speeds, and environmental requirements.
Our technical engineers analyze your product's moisture profile, packaging geometry, and line vibration levels to configure custom aperture dimensions, multi-frequency software algorithms, and dedicated rejection mechanisms (including pneumatic pushers, air jets, or drop-out belts). From initial pre-sales consulting and ROI analysis to remote technical support and lifecycle maintenance, SameGram stands beside your operational team at every stage.
Ready to eliminate false rejects and secure your line against real-world contaminants?
Contact our application engineering team today to arrange a complimentary product sample evaluation and receive a customized aperture-and-sensitivity calculation for your production line.
Author Profile & Signature
Author: Tony, Founder & CTO, SameGram.
“At SameGram, every innovation starts with listening — to machines, to data, and most importantly, to our customers.”
Hot-Sale Conveyor Metal Detector
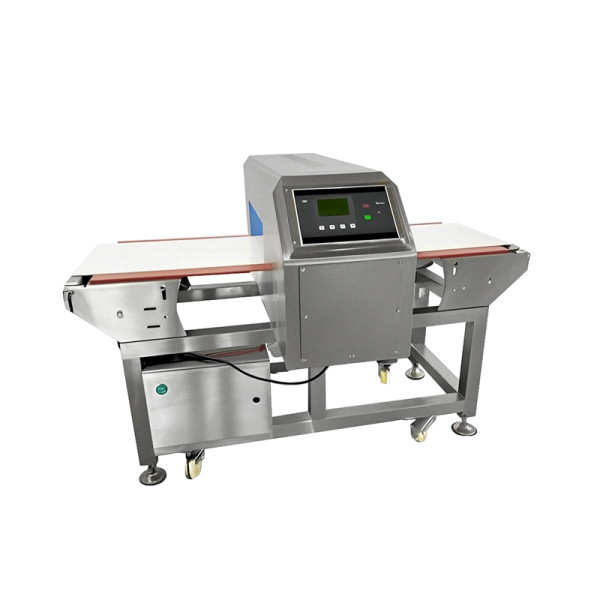
DD-720 is a belt conveyor metal detector with unmatched sensitivity, ideal for food and pharma.
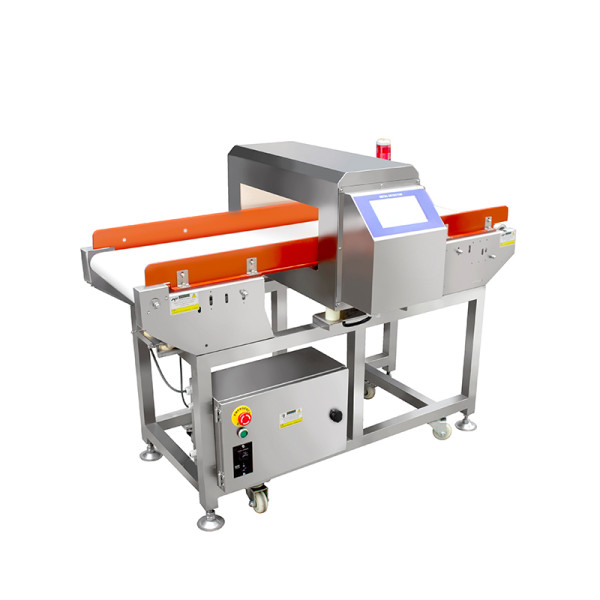
DD-500 Series is an advanced conveyor belt metal detector using smart touch-screen control. Ideal for food production and other
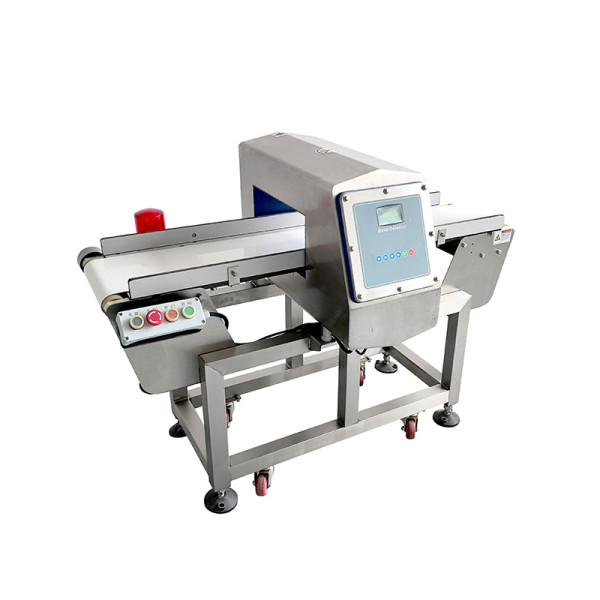
Customizable metal detector for conveyor belt with dual frequency, high sensitivity, and strong anti-interference.
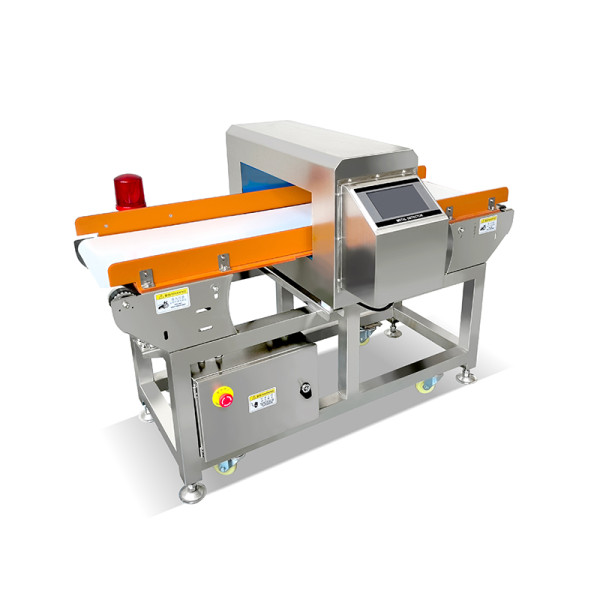
DD-360 Series is a food-grade metal detector conveyor system. Ideal for food industry and food production lines.
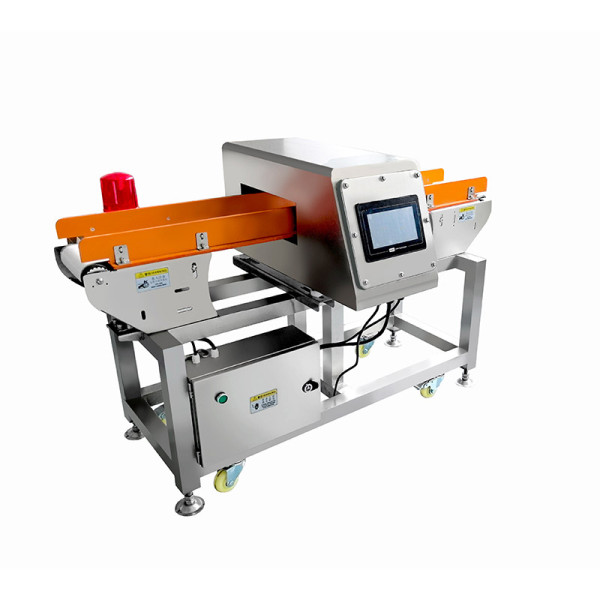
DD-220 is a food conveyor metal detector designed for aluminum foil packaging,with high sensitivity and easy integration.